Chemicals for aerospace and defense

Degreasing solvents, passivation and anodizing acids, conversion chemicals and wipe solvents for manufacturing, MRO and depot maintenance.

Every size listed is priced and sold online, with no minimum. Quotes are for multi-unit, bulk and recurring supply. Or call 512-365-6838.

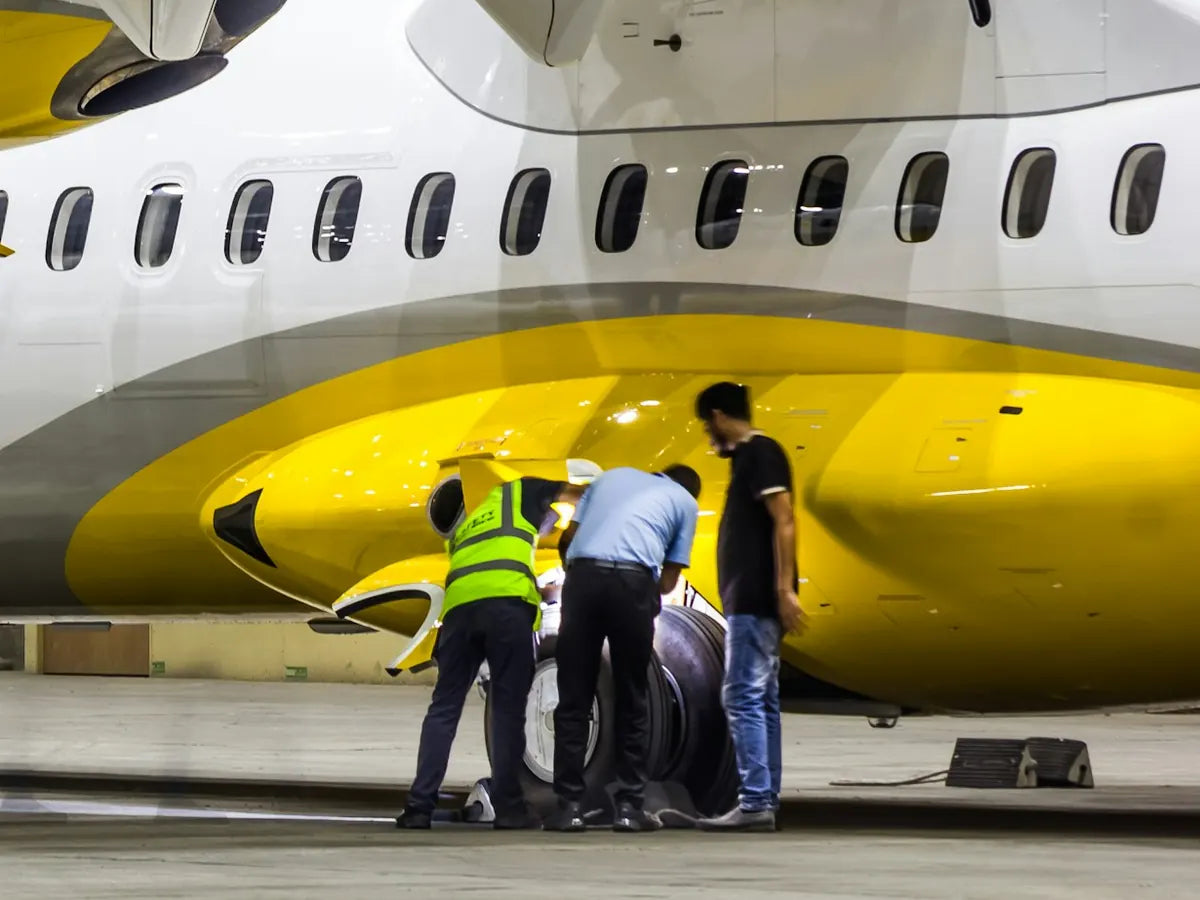
Technicians inspecting an aircraft's landing gear in a hangar

Photo: Bornil Amin on Unsplash

Where the chemistry goes

Surface preparation in four steps, the way most specifications sequence it. Government buyers can find our CAGE code and NSN directory on the Government page.

  1. Step 1 Degreasing

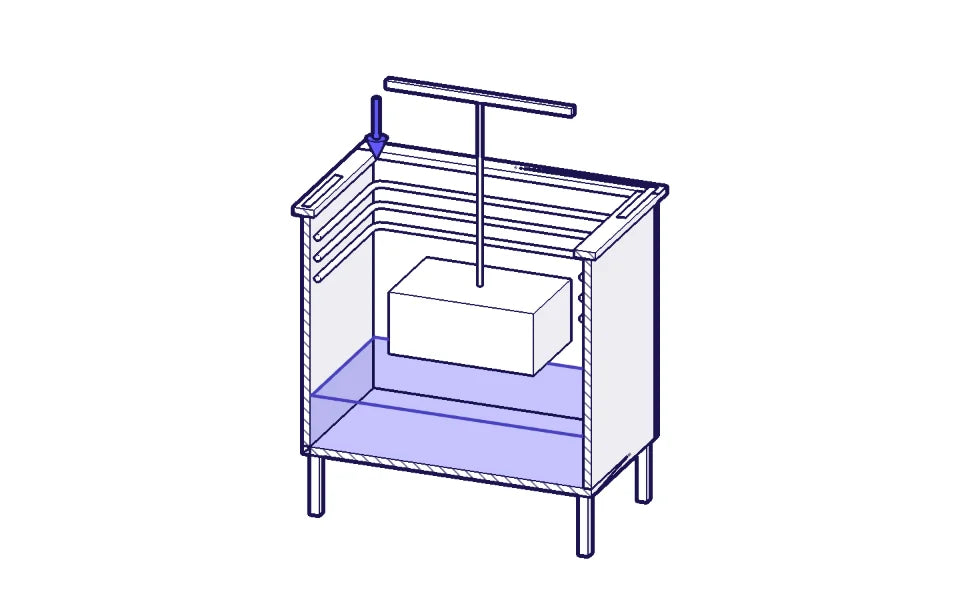
    Vapor degreaser, cut away

    Parts come off the machine with oils and coolant that have to go before any surface treatment. A petroleum solvent wash does most general cleaning; chlorinated vapor degreasing is now limited by EPA rules to specific exempted uses.

  2. Step 2 Passivation

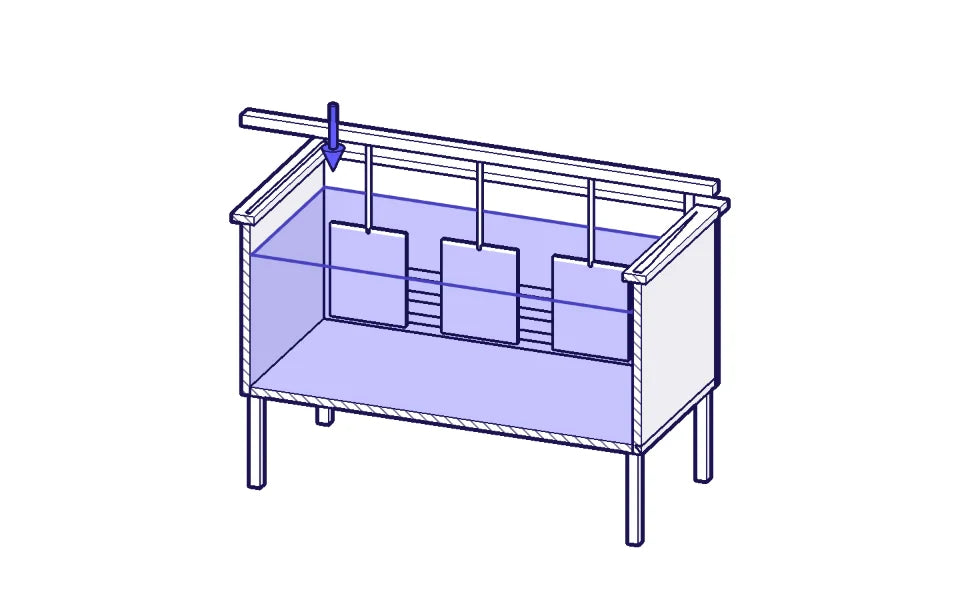
    Passivation bath with parts on a flight bar, cut away

    Passivation removes free iron from stainless steel so its chromium oxide layer can form. Nitric acid is the traditional bath; citric acid is the lower-hazard alternative most specifications now allow.

  3. Step 3 Anodizing and conversion

    Anodizing tank, cut away

    Aluminum is anodized in sulfuric acid to build a protective oxide, then sealed. Phosphoric acid anodize builds a thin, porous oxide that is left unsealed as a base for adhesive bonding. Dichromate seals and conversion coatings still appear on legacy drawings.

  4. Step 4 Wipe before bonding and paint

    Solvent wipe set-up

    Immediately before bonding, sealing or painting, a solvent wipe removes fingerprints and residue. Ketones and isopropyl alcohol flash off fast and leave little residue.

Technical notes

Reference notes on the specifications, standards, regulations and paperwork that matter when you source surface preparation chemicals for aerospace manufacturing, MRO and defense work.

Key specifications

Specification Why it matters
Specification conformance Many defense and aerospace drawings name a commercial item description, military specification or AMS number. Buy to the named document and revision, and confirm the product states conformance to it.
Assay / purity (%) Passivation, anodizing and conversion baths are made up to set concentrations, and an off-assay lot shifts the result. A known assay keeps the bath inside the specification's limits.
Trace metals and chloride (ppm) Chloride and some metals attack stainless steel and aluminum alloys or disturb oxide growth. Check the impurities that matter for your alloy on the lot's COA.
Shelf life and date of manufacture Defense contracts and quality systems often limit how old material can be at receipt. Ask about the lot's age before you order a large quantity.
Lot traceability Audits trace a part back to the chemical lots used on it. A COA for the lot you receive is free on request; file it with the lot number from the label.

Industry overview

Aerospace and defense surface preparation follows a familiar sequence: degrease, passivate or pickle, anodize or convert, then wipe clean immediately before bonding, sealing or painting. Manufacturing, MRO and depot maintenance shops use A-A-59601E Type III high-flash petroleum cleaning solvent for general parts cleaning, nitric or citric acid to passivate stainless steel, sulfuric acid to anodize aluminum, phosphoric acid anodize ahead of adhesive bonding, and MEK, acetone or isopropyl alcohol as wipe solvents. Trichloroethylene vapor degreasing is now limited to narrow EPA exemptions, while perchloroethylene degreasing continues under EPA workplace controls.

What separates this work from general industry is the paperwork. Drawings call out ASTM A967, AMS 2700, MIL-PRF-8625 or MIL-DTL-5541, and each part has to trace back to the chemical lots used on it. Government buyers need the supplier's CAGE code and UEI for an award. Alliance Chemical holds CAGE 1LT50 and supplies about 227 NSNs in three supply classes, listed on our government buying page.
Why grade matters

Grade questions in aerospace are mostly about residue and impurities. ACS reagent isopropyl alcohol 99.9% suits optics, sensors and electronics because it evaporates with very little non-volatile residue; a lower-grade solvent may leave a film that shows up as glare or a failed bond. Passivation specifications such as ASTM A967 and AMS 2700 set bath concentration, temperature, time and verification tests rather than naming a reagent grade, so a low-particle or ACS grade nitric acid is a choice some shops make for precision parts, not a standing requirement. In sulfuric acid anodizing to MIL-PRF-8625, iron and other impurities in the acid build up in the bath and can produce an uneven or discolored coating that struggles in salt spray testing. Match the grade to the step and the drawing.

Regulations to know

Stainless steel passivation is usually specified to ASTM A967 or AMS 2700, sulfuric acid anodizing to MIL-PRF-8625, and chromate conversion coatings to MIL-DTL-5541. Hexavalent chromium from sodium dichromate brings the OSHA chromium (VI) standard, with exposure monitoring and medical surveillance. OSHA exposure limits govern ventilation for solvent wiping and acid tanks. EPA rules finalized in December 2024 prohibit most uses of trichloroethylene, with time-limited exemptions that include batch vapor degreasing of essential aerospace parts. Perchloroethylene vapor degreasing can continue under EPA workplace exposure controls. Both rules are under legal challenge and EPA review, so confirm the current status before you order. Shops working to AS9100 or under DCMA oversight need lot traceability on purchased chemicals. To sell to the government, a supplier needs an active SAM registration with a CAGE code and UEI; ours are 1LT50 and DCTCZDY3BLD3.

Common purchasing mistakes

  • Wiping with a solvent that leaves residue. A ketone carrying trace oil or high non-volatile residue, used immediately before bonding, can cause adhesive or coating failure. Check NVR on the COA.
  • Making up a dichromate seal without the lot assay. An off-strength seal bath gives uneven color and weaker corrosion resistance on anodized aluminum. An off-strength bath gives a powdery, poorly adherent coating on aluminum.
  • Finding the paperwork gap at receiving. If the COA does not report the tests your quality plan requires, the lot is quarantined and the line waits. Ask for a current COA and compare it with your requirements before you order.
  • Ordering TCE or PCE for a use the EPA rules no longer allow. Confirm that the use qualifies before the drum ships.

Shipped from Taylor, Texas

Most in-stock orders leave in one to two business days. Parcel or freight depends on what is in the box, not on who is buying, and every size listed is sold online.

UPS Ground Bottles, jugs and up to three pails
LTL freight Four or more pails, drums and totes, by liftgate truck on a pallet
  • UPS
  • ABF Freight
  • FedEx Freight
  • R+L Carriers
  • Saia
  • Southeastern Freight Lines
  • XPO

The carrier's hazmat fee is passed through at cost. See the shipping guide for how orders are packed and rated.

Questions buyers ask

What is A-A-59601E Type III?

It is a commercial item description for petroleum cleaning solvent, the successor to P-D-680. Type III is the high-flash-point type, used for general parts cleaning in military and aerospace maintenance. The product page lists the CAS number and shipping name.

Nitric or citric acid for passivation?

Both remove free iron from stainless steel. Nitric is the older bath and works on more alloys; citric is less hazardous to handle and dispose of. Follow the method your drawing or specification calls out.

Can government buyers order with a purchase card?

Yes. Card orders go through the normal checkout. Purchase orders can be emailed to sales@alliancechemical.com, and our CAGE code is 1LT50.

Do you send a certificate of analysis?

A COA for the lot you receive is free on request, and safety data sheets for every product are in the SDS library.

What are Alliance Chemical's CAGE code and UEI?

Our CAGE code is 1LT50 and our UEI is DCTCZDY3BLD3. Both are on our government buying page, along with our NSN directory.

Can Alliance Chemical bid on set-aside contracts?

Alliance Chemical is woman-owned, registered in SAM.gov under CAGE 1LT50, and supplies about 227 NSNs in three supply classes. Check our current certifications in the SAM.gov and SBA records before award.

Which standards cover stainless steel passivation?

ASTM A967 and AMS 2700 are the common ones. Both define nitric and citric acid treatments by concentration, temperature and time, plus the tests that verify the result, so follow the method your drawing calls out.

What documentation supports an AS9100 or DCMA audit?

An SDS for every product and a COA for the lot you receive, free on request. The lot number on the container ties the two together in your traceability file.

Do you sell trichloroethylene for vapor degreasing?

We sell TCE, but EPA TSCA rules finalized in late 2024 restrict its use to narrow exemptions. Confirm that your degreasing use still qualifies before you order.

Which isopropyl alcohol suits optics and sensor cleaning?

Isopropyl alcohol 99.9% ACS reagent grade. It evaporates quickly with very little residue, which is what optics, sensors and electronics need.

Order today, or talk it through first

Every size listed on this page is priced and sold online. For drums and totes on a schedule, several delivery points or net 30 terms, send us your volumes and we will quote the product and the freight.

Call sales 512-365-6838

Monday to Thursday 8 am to 4 pm, Friday 8 am to noon, Central time